

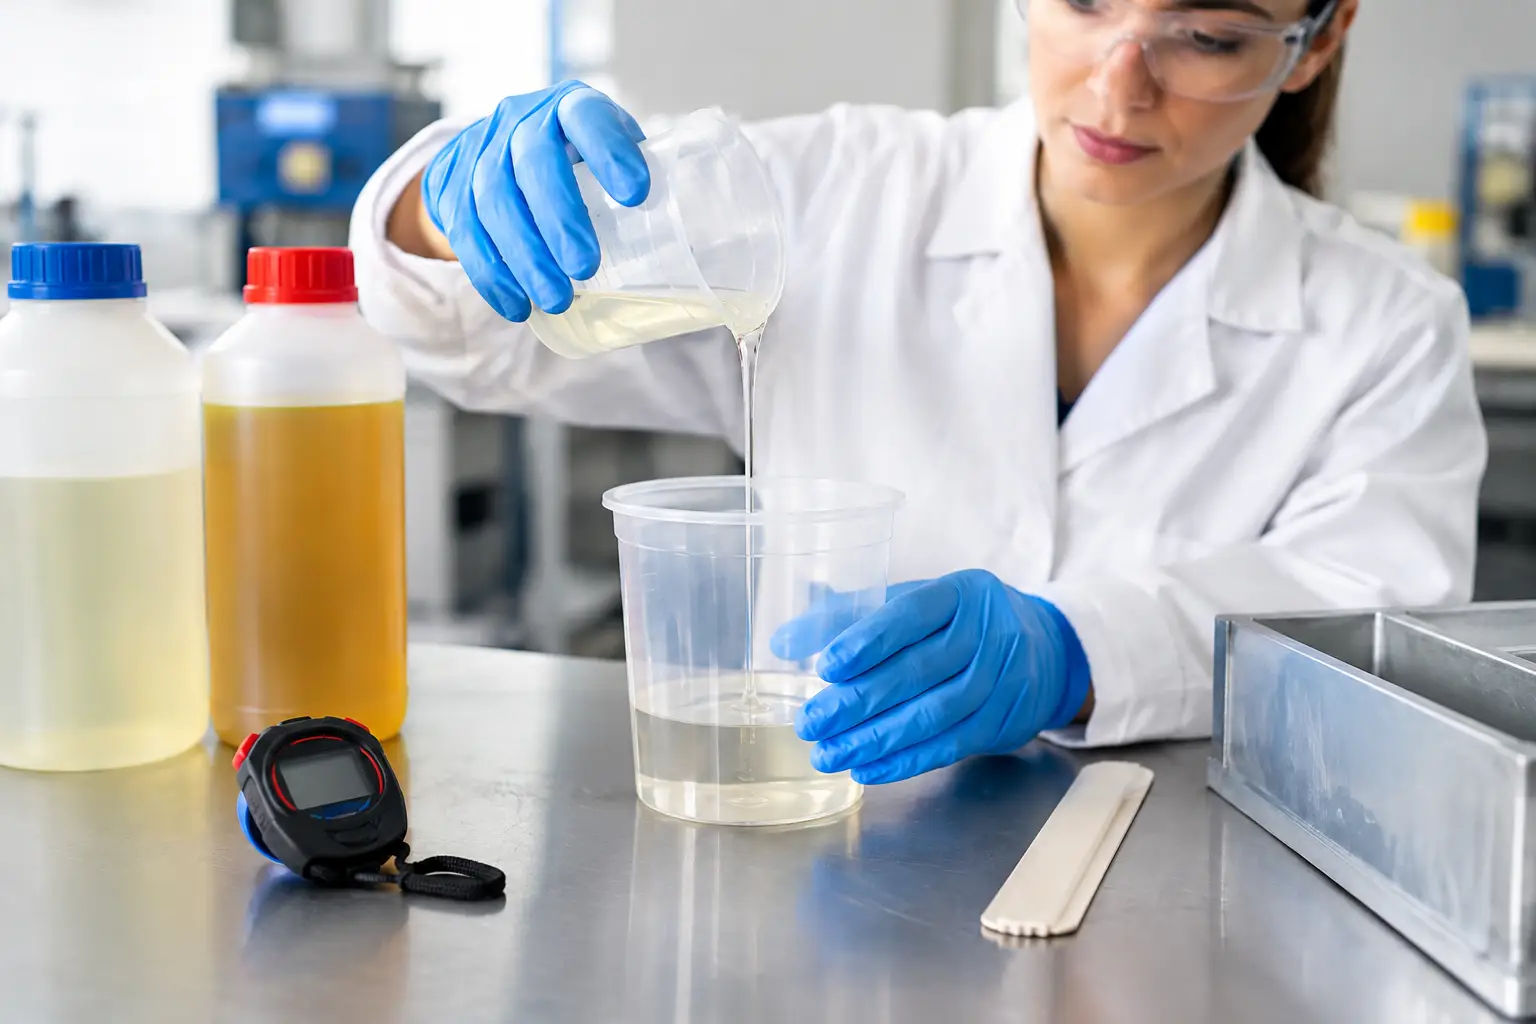
A batch can look correct at the mixing station and still fail on the production floor if its workable time is misunderstood. Epoxy pot life measurement gives formulators and production teams a defined processing window after resin and hardener are combined, helping them schedule mixing, application, impregnation, and cleanup before viscosity rises beyond a usable level.
For industrial epoxy systems, pot life is not simply a catalog value. It changes with resin grade, curing-agent chemistry, accelerator level, batch size, filler loading, mixing energy, and actual shop temperature. A reliable measurement method turns that variable behavior into a specification that purchasing, formulation, and production teams can use.
What Epoxy Pot Life Actually Measures
Pot life is the time during which a mixed epoxy formulation remains workable under stated conditions. “Workable” must be defined for the process. For a coating, it may mean the point at which spray viscosity becomes too high or leveling declines. For an electrical encapsulant, it may be the limit for vacuum degassing and complete cavity fill. In a composite process, it can be the time available for fiber wet-out and laminate consolidation.
The chemical cause is the same: once epoxy resin and curing agent are mixed, molecular weight begins to build. The system thickens, heat may be generated, and flow changes. Eventually, the material gels and can no longer be processed effectively.
Pot life is often confused with gel time, but they should not be treated as interchangeable. Gel time is the point at which the material forms a continuous network and loses fluidity. Pot life is usually earlier because a formulation may become too viscous for the intended application well before gelation. For production control, the more useful number is often the process-specific limit rather than the final gel point.
Why Pot Life Must Be Measured Under Controlled Conditions
A quoted pot life without temperature, mix quantity, and endpoint is incomplete. Epoxy cure reactions are temperature-sensitive. A formulation that remains usable for several hours at 77°F may have a much shorter working window at 95°F in a summer production area.
Sample mass matters as well. Epoxy curing is exothermic, meaning the reaction releases heat. A small laboratory cup can shed heat quickly, while a large container retains it. The retained heat accelerates reaction, which creates more heat and shortens pot life further. This is why a 100-gram test cannot automatically predict the behavior of a 20-kilogram batch.
The test container, ambient conditions, and agitation method also affect the result. A deep cup retains more heat than a shallow tray. Continuous agitation can delay local heat buildup but may change the practical result for a process that uses static material. Good measurement does not eliminate these variables. It identifies and controls them.
A Practical Method for Epoxy Pot Life Measurement
The most useful approach is to test the exact resin-hardener formulation at a defined batch size and temperature, then select an endpoint that matches the actual operation. This makes the result meaningful for release testing and scale-up decisions.
Prepare the Materials and Conditions
Condition the resin, hardener, fillers, and additives at the selected test temperature before mixing. Record the room temperature and, where relevant, relative humidity. For moisture-sensitive curing agents or electrically demanding applications, controlling moisture exposure may be necessary as well.
Use calibrated scales and mix at the specified stoichiometric ratio. A ratio error can change cure speed, viscosity development, and final properties. If the production process uses a defoamer, accelerator, pigment paste, fumed silica, or other additive, include it at the intended use level. Measuring a simplified laboratory blend may produce a result that does not reflect the supplied formulation.
Select a sample mass that represents the process risk. A small, repeatable sample is suitable for lot-to-lot comparison. A larger sample or a separate scale-up trial is needed when evaluating exotherm in bulk mixing, casting, or electrical potting.
Start Timing at the End of Mixing
Begin the timer immediately after the components are fully blended. Use a consistent mixing method and duration for every test. Incomplete mixing can give an artificially long pot life in one area of the sample and a short, uneven cure in another.
Record the initial viscosity, appearance, and temperature. These baseline values are valuable when investigating changes between resin lots, hardener lots, or supplier alternatives.
Monitor the Chosen Endpoint
For many liquid systems, viscosity is the best endpoint. Measure viscosity at fixed intervals using the same instrument, spindle, speed, and sample temperature. Pot life can be reported as the time required to reach a defined viscosity, such as the maximum viscosity permitted by spray equipment, dispensing pumps, or impregnation equipment.
A simpler shop-floor approach is a periodic flow check or stirring resistance observation, provided the method is written clearly. The operator must know what constitutes the endpoint. “Too thick to use” is not a controlled specification. “No longer flows through a specified orifice within the stated time” is much more repeatable.
Track sample temperature throughout the test, especially for fast-reacting amine-cured systems, filled compounds, and larger batch sizes. A rapid temperature rise often signals approaching runaway exotherm and can explain why the usable window collapses faster than expected.
Record More Than One Result
A complete test record should include the resin and hardener identification, mix ratio, additive package, sample mass, container geometry, start temperature, ambient temperature, mixing procedure, viscosity method, endpoint definition, pot life result, gel time if measured, and peak sample temperature.
This information allows the result to be compared later. It also helps a procurement team determine whether a reported difference is caused by raw material variation or by a change in test conditions.
Selecting the Right Endpoint by Application
There is no single pot life endpoint that suits every epoxy system. The correct specification depends on what the material must do before cure.
For protective coatings and flooring, the practical endpoint is usually tied to application viscosity, wet-edge performance, or film appearance. A system may still be liquid after it has lost acceptable leveling or begins to produce orange peel, poor wetting, or inconsistent film thickness.
For structural adhesives, dispense consistency and substrate wetting are key. The material must remain fluid enough to achieve the required bond-line thickness and assembly time. A longer pot life can help with large assemblies, but it may also delay fixture release and reduce production throughput.
For composites, pot life needs to support wet-out, resin transfer, layup, vacuum processing, and consolidation. Low-viscosity anhydride-cured epoxy systems are often selected where extended processing time and electrical performance are required, but their cure schedule must be matched carefully to the manufacturing cycle.
For electrical encapsulation and insulation, the window includes mixing, vacuum degassing, dispensing, and complete filling before viscosity prevents bubble release or creates voids. Here, viscosity change and exotherm are often more useful controls than a single visual gel test.
Common Reasons Pot Life Results Do Not Match Production
When laboratory and plant results differ, temperature is usually the first factor to check. Material stored in a warm warehouse, a heated production line, or direct sunlight can begin the process several degrees above the stated test condition. That difference can be enough to shorten the usable window significantly.
The second common cause is batch size. A larger mix retains heat and reacts faster. This is particularly relevant when a system moves from small manual mixes to drums, totes, static mixing equipment, or large potting vessels.
Accelerator level is another major lever. Tertiary amines, imidazoles, and other epoxy accelerators can improve cure speed or reduce oven time, but even a small dosage change can reduce pot life. The same applies to reactive diluents, fillers, pigments, and moisture-containing raw materials. Each formulation adjustment should be checked against both workable life and final cured performance.
Raw material compatibility also matters. Resin epoxy equivalent weight, hardener acidity or amine value, viscosity, and impurity profile influence cure behavior. Consistent sourcing is therefore part of process control, not only a purchasing decision.
Using Pot Life Data for Better Material Sourcing
For a buyer, the most useful supplier data includes more than a nominal pot life value. Ask for the stated test temperature, batch mass, resin-hardener ratio, method, and endpoint. If the formulation will run in a high-volume operation, request samples for validation using the actual fillers, pigments, accelerators, and equipment conditions.
Dahua New Materials supplies liquid epoxy resins, MTHPA hardeners, amine and polyamide curing agents, accelerators, and formulation additives for industrial epoxy systems. Matching these materials is not only about achieving cure. It is about establishing a predictable processing window that supports production yield, equipment capability, and shipment planning.
A well-defined pot life specification gives operators a clear decision point: mix only the quantity that can be applied, impregnated, or dispensed within the validated window. That simple discipline protects material value, reduces avoidable scrap, and makes every batch easier to run with confidence.